
 +39 0535 74 01 11


Engineering Performance, Ensuring Safety: WAMGROUP’s Specialised Solutions for the Food and Agricultural Markets
For almost 60 years, WAMGROUP has been a benchmark in bulk solids handling and processing technology, offering smart, sector-specific equipment solutions that align with the market needs of producers and processors worldwide.
Engineered for Industry-Specific Challenges
From the delicate handling of flour in bakery lines to the controlled feeding of additives in feed production or the transfer of mineral blends in fertilizer plants, WAMGROUP develops machines that are as precise as they are robust. Central to this approach is a deep understanding of market-specific priorities: hygiene and traceability in food processing, flow consistency in feed, and abrasion resistance in fertilizer applications.
The company’s equipment—such as screw conveyors, rotary valves, butterfly valves, micro-batch feeders, bin activators, dust collectors, and FIBC dischargers—is designed with modularity in mind. This enables quick adaptation to a wide variety of process layouts, material properties, and regulatory standards, particularly in sectors where product integrity and plant efficiency go hand in hand.
Cleanability, Compliance, and Continuous Flow
For industries where contamination or downtime can severely impact operations, WAMGROUP’s engineering choices make a measurable difference. Stainless steel components, hygienic design principles, and easy-access maintenance features are standard across food-grade equipment lines. These characteristics allow operators to meet strict food safety regulations while reducing cleaning time and minimising interruptions.
In animal feed and fertilizer production, material flow can be unpredictable and abrasive. WAMGROUP addresses this with purpose-built screw conveyors, feeders, and conditioning systems that ensure high wear resistance, low maintenance needs, and consistent throughput—even in challenging environments.
Clean Air, Safer Processes: Dust Collectors in the Spotlight
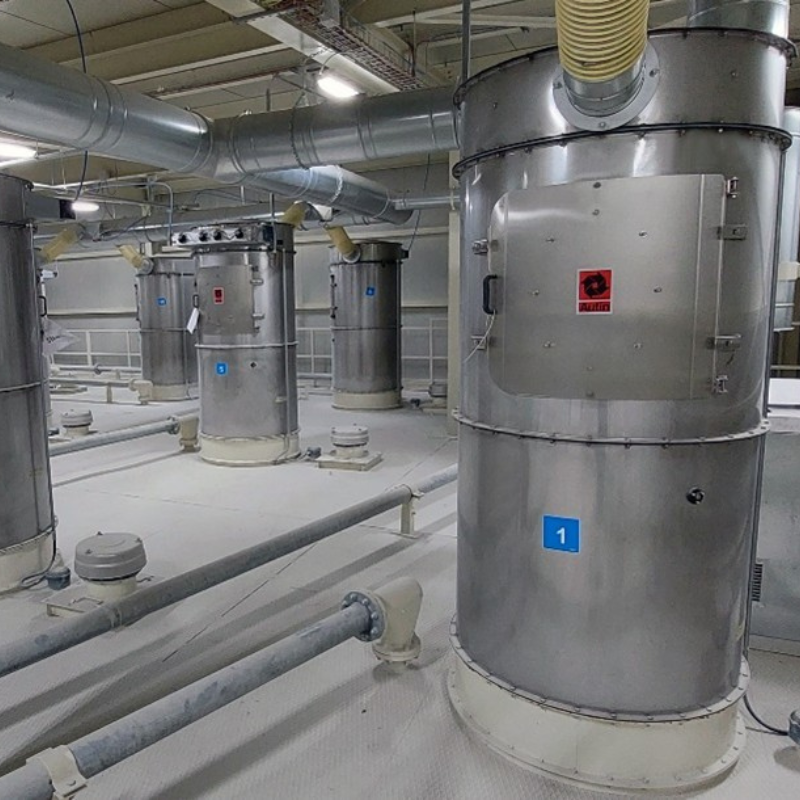
In both food and feed plants, airborne dust is more than just a housekeeping concern—it’s a potential risk to product quality, operator safety, and regulatory compliance. WAMGROUP’s dust collectors for food and feed applications are specifically engineered to address these challenges.
Equipped with high-efficiency filtration elements and designed in accordance with ATEX directives where required, these systems ensure safe air quality while preventing cross-contamination. Compact footprints, modular construction, and stainless-steel options make them ideal for integration into hygienic environments, from flour milling to feed pelletising.
“Dust control is not just about compliance—it’s about protecting the product, the people, and the plant,” explains a WAM AIR filter division product manager. “Our food- and feed-grade dust collectors are designed for easy maintenance, quick filter replacement, and maximum filtration efficiency, ensuring that airborne particles never compromise process integrity.”
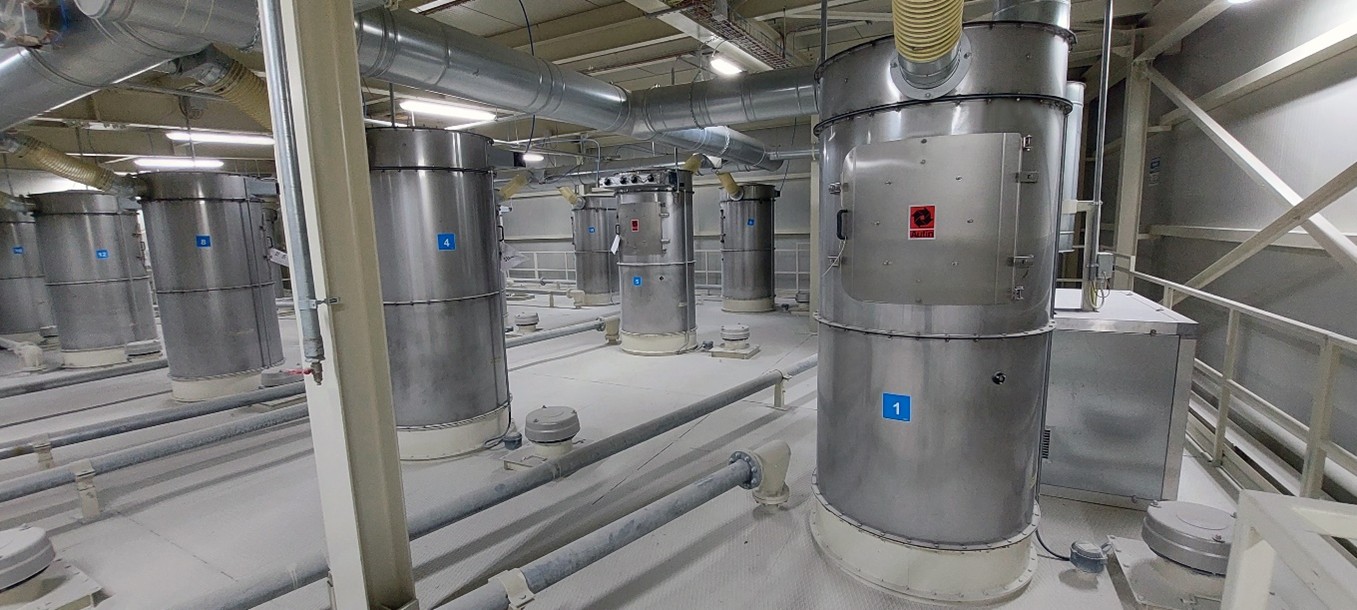
By keeping production areas cleaner and safer, these dust collectors contribute directly to higher product quality, reduced downtime, and improved overall equipment effectiveness (OEE)—key metrics for competitive, high-volume operations.
Critical Role of FIBC Discharging Systems
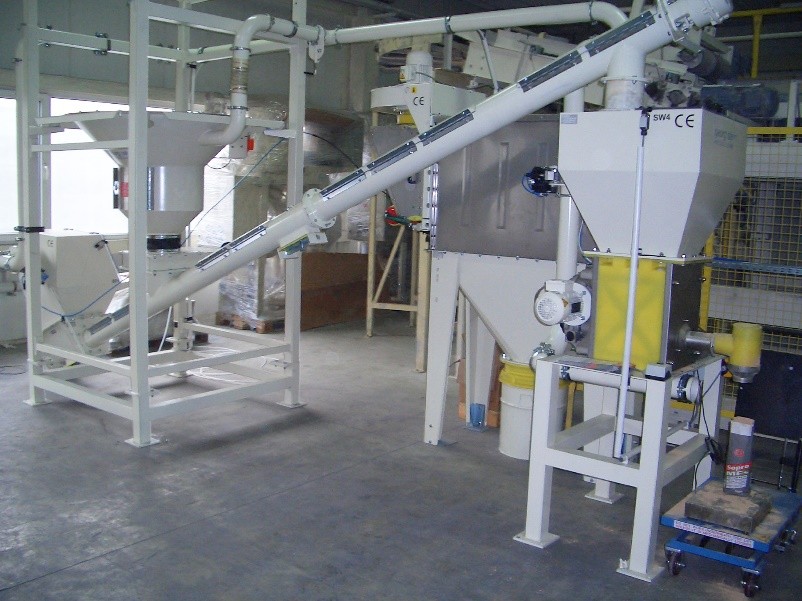
An essential piece of the puzzle in both food and agricultural processes is the safe and efficient discharging of bulk ingredients. WAMGROUP’s FIBC dischargers—specifically the SBB-HFF (with high-flow rate for poor-flowing powders) and the SBB-ADS (with anti-dust system)—offer manufacturers an optimal solution for handling bulk bags.
These units are engineered for high flow rates, minimal product residue, and safe operation. They are particularly effective when integrated into automated feeding lines, enabling clean and controlled transfer of materials from bulk bags into downstream equipment. With growing demand for traceability and contamination prevention, especially in food and feed applications, these dischargers play a vital role in maintaining process integrity and operator safety.
SEPCOM®: Enabling Circular Agriculture
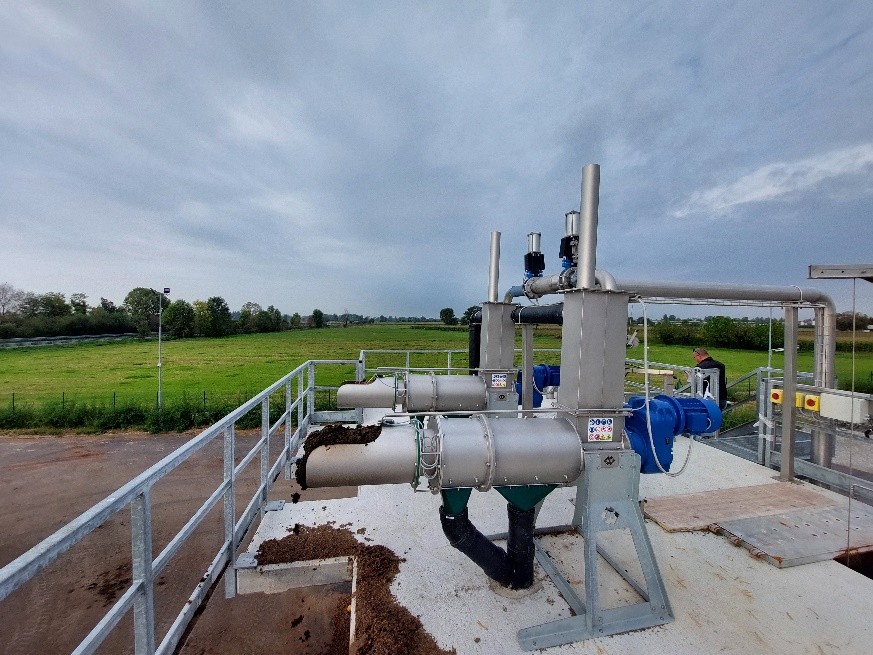
In parallel with traditional equipment, WAMGROUP has pioneered innovation in the field of organic waste valorisation with its SEPCOM® range. These compact solids-liquid separators are designed to process livestock manure, digestate, and food processing residues—transforming organic waste into manageable resources.
By separating solids and liquid fractions, SEPCOM® units support nutrient management, reduce transport and storage volumes, and enable downstream uses like composting, fertigation, or energy production. The system’s screw press technology delivers consistent separation even in fibrous or variable-content materials, making it a reliable choice for farms, cooperatives, and agro-industrial plants aiming to reduce their environmental footprint.
From Plant Floor to Market Impact
What sets WAMGROUP apart is not only its technical breadth, but its commitment to customer outcomes. With a global network of subsidiaries, the company offers proximity and responsiveness, from equipment selection and process design to post-installation support.
“In our target markets, the focus is not only on mechanical performance but also on hygiene, compliance, and total cost of ownership,” says the WAMGROUP Sales Manager for Agricultural Applications. “We design equipment with the customer’s production goals in mind.”
A Strategic Partner for a Smarter Future
In a time when food safety, environmental sustainability, and production efficiency are at the heart of every investment decision, WAMGROUP’s specialised solutions empower customers to stay ahead. Whether it's in flour handling, animal feed feeding, fertilizer production, dust control, or waste valorisation with SEPCOM®, the company continues to deliver equipment that performs—so customers can focus on what matters most: quality, productivity, and growth.


